ZTF Forming Process


Product sourcing details
- Place of Origin
- China (Mainland)
- Packaging
- as your demand
Supplier: Shijiazhuang Zhongtai Pipe Technology Development Co.,Ltd
Purchasing information
- Minimum order
- 1
- Lead time
- 60 Days
Please confirm with the supplier: Model / reference, Key specifications / compatibility, Samples, Export markets, Supply capacity.
Specifications
Description
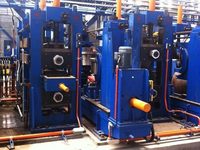
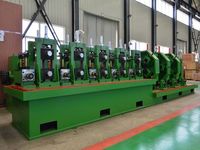
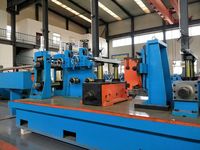
ZTF forming process
- Do not need to change moulds in breakdown section, saving about 60% cost on the rolls
- Roll changing time is cut down greatly, breakdown section does not need to change moulds and just adjust is ok. And it can cut-down producing period.
- Release labor intensity.
- Roll forming technology, the caliber is different and propitious for X70,N80 steel strip.
6)It is easier to restore and adjust roller.
II.Where is ZTF used?
ZTF technology is used in breakdown section and only suit to produce round pipes.
III.What is breakdown section and what is fin-pass section?
Normally, we part the mills as forming section and sizing section.
The section before guild-frame is forming and the rest part is sizing section.
For ZTF, we divide forming section into breakdown section and fin-pass section. The part after the unit of vertical rolls is fin-pass section and before is breakdown section.
VI.The development of ZTF technology
The Comparation Among Four Generations of Our Pipe Forming Technology
“ZTF-1”, “ZTF-2” , “XZTF-3” and “XZTF-4”
| Technology | ZTF-1 | ZTF-2 | XZTF-3 | XZTF-4 |
| Adjustment Method | Manual | Manual | Electric | Electric |
| Rolls in Breakdown section | Basically Common Use | Fully Common Use | Fully Common Use | Fully Common Use |
| Structure and Adjustment of Rotating Horizontal Rolls | No Horizontal Rolls | Manually adjust the rotating, opening & closing and lifting of upper rolls, the lower rolls opening& closing on the shaft. Manually adjust quick release or adjustable mats. | Electric adjust the rotating, opening & closing and lifting of upper rolls , tilting lower rolls opeing& closing on the roll seats. Electric adjust the the space between rolls which is controlled by screw. | Electric adjust the rotating, opening & closing and lifting of upper rolls. Computer adjust the tilting of the lower rolls opening& closing on the roll seats, the space between rolls which is controlled by screw |
| Structure and Adjustment of Swiveling Vertical Rolls | Manually control the adjustment for the opening & closeing, lifting and rotating of the special curve rolls. | Manually or electromotion control the adjustment for the opening & closing, lifting and rotating of the special curve rolls. | Electric control the adjustment for the opening & closeing, lifting and rotating of the special curve rolls. | Computer control the adjustment for the opening & closeing, lifting and rotating of the special curve rolls. |
| Adjustment of Other Rolls in Roughly Forming Section | Rollers shall be replaced when producing new size of pipe. | The rolls open and close on the shaft, manually adjust the quick release and the adjustable mats, the lifting the upper rolls. | The rolls open and close on the shaft or roll seats, manually adjust the space between rolls which is controlled by screw, the lifting of the upper rolls. | The rolls open and close on the shaft or roll seat. Electric adjust the space between rolls which is controlled by screw. Computer adjust the lifting of the upper rolls. |
| Micro-adjustment Device for Side Vertical Rolls in Final Forming and Sizing Section | N/A | N/A | Yes | Yes |
| Adjustment for Rolls Position | Manual | Manual | Manual | Computer |
| Request for Electronic Control | Low | Low | High | Higher |
| Accuracy of Rolls Position Adjustment | High | High | Higher | Highest |
| Operation Site of Rolls position Adjustment | Inside the stands | Inside the stands | Outside the stands | Outside the stands |
| Deformation of the Pipe Blank Edge | Good | Good | Better | Better |
| The Formation for High Rrecision, High Steel Grade and Thick Wall Pipe | Good | Better | Best | Best |
| Accuracy of Pipe | High | High | Higher | Higher |
| Labour Intensity | High | High | Low | Very low |
| Time for Replacing Rolls | Long | Short | Short | Shortest |
| Online Adjustment | Normal | Normal | Good | Good |
| Model | Round pipe mm | Square pipe mm | Thickness mm | Working spead m/min |
| ERW114 | Ф48-Ф114 | 40x40-90x90 | 1.5-4.5 | 65 |
| ERW140 | Ф60-Ф140 | 50x50-110x110 | 2.0-5.0 | 60 |
| ERW165 | Ф76-Ф165 | 60x60-130x130 | 2.0-6.0 | 50 |
| ERW219 | Ф89-Ф219 | 70x70-170x170 | 2.0-8.0 | 50 |
| ERW273 | Ф114-Ф273 | 90x90-210x210 | 3.0-10.0 | 45 |
| ERW325 | Ф140-Ф325 | 110x110-250x250 | 4.0-12.7 | 40 |
| ERW377 | Ф165-Ф377 | 130x130-280x280 | 4.0-14.0 | 35 |
| ERW406 | Ф219-Ф406 | 170x170-330x330 | 6.0-16.0 | 30 |
| ERW508 | Ф273-Ф508 | 210x210-400x400 | 6.0-18.0 | 25 |
| ERW660 | Ф325-Ф660 | 250x250-500x500 | 6.0-20.0 | 20 |
| ERW720 | Ф355-Ф720 | 300x300-600x600 | 6.0-22.0 | 20 |
- Company: Shijiazhuang Zhongtai Pipe Technology Development Co.,Ltd
- Contact: Kathleen Zhen